Live OEE vs OEE from a Spreadsheet: the Hidden Cost of Manual Measurement
DBR77 Team · Published
Live OEE is calculated continuously from machine events, so it shows losses while the shift can still act on them. Spreadsheet OEE is rebuilt by hand after the fact, usually misses short stops and guessed reasons, and arrives a day too late to change anything.
Both use the same formula. They differ in their inputs and timing, and that gap costs more than most plants assume.
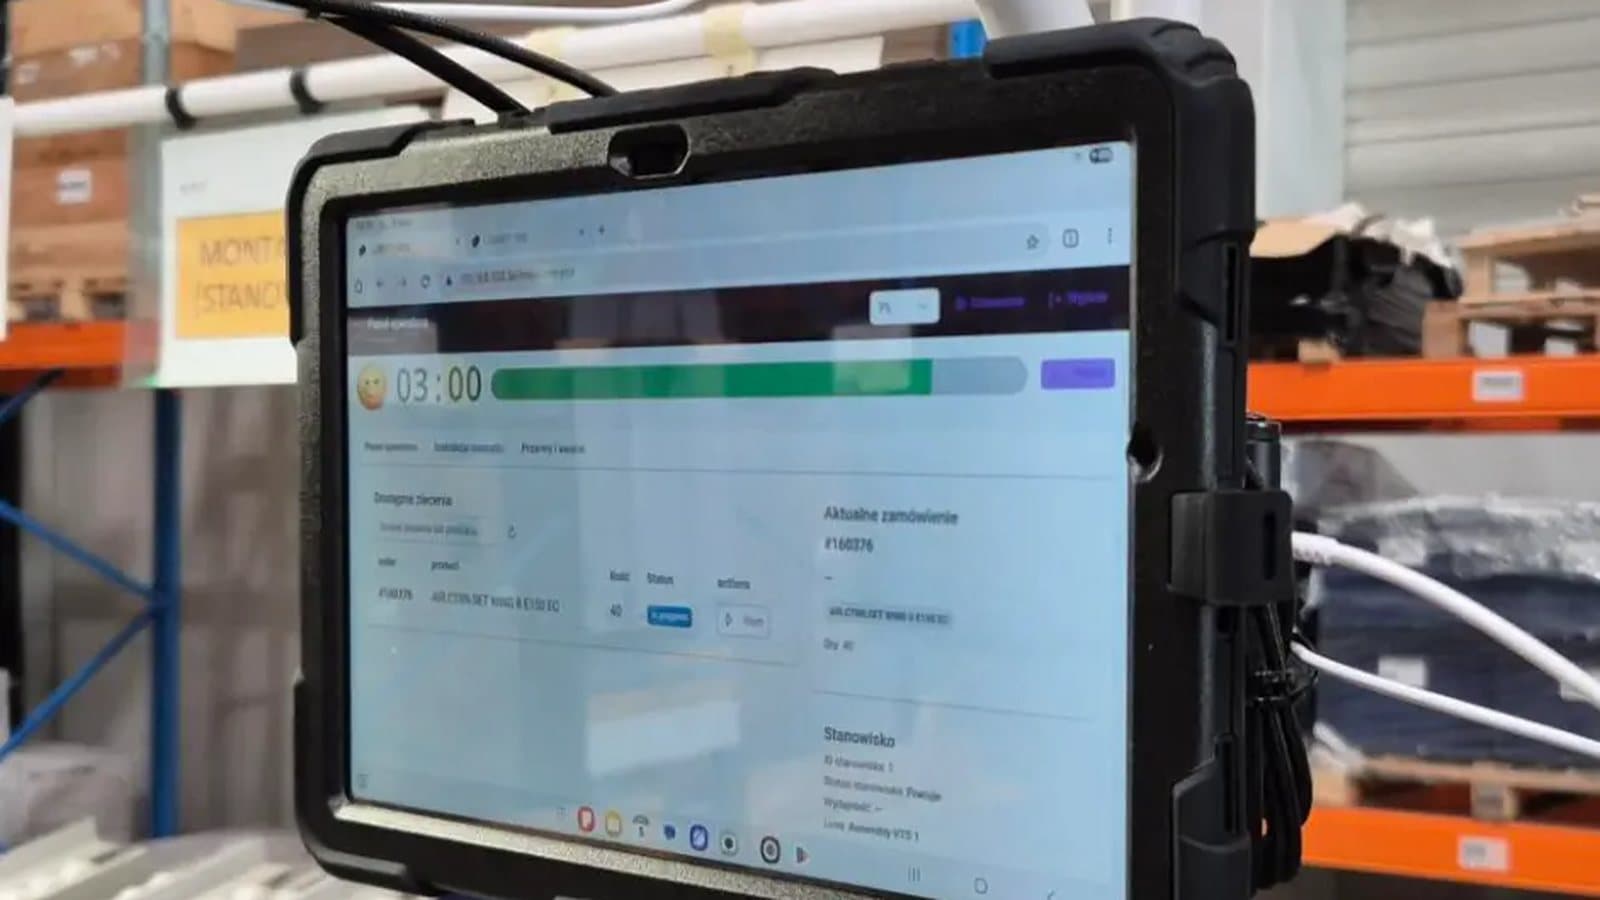
How OEE is calculated
OEE (overall equipment effectiveness) multiplies three factors:
OEE = Availability × Performance × Quality
- Availability is run time divided by planned production time.
- Performance is ideal cycle time × total count, divided by run time.
- Quality is good count divided by total count.
Vorne's worked example for one shift gives 88.81% availability, 86.11% performance and 97.80% quality, so OEE is 74.79%. It also defines planned production time as shift length minus breaks.
For context, 85% is often cited as world class, while most manufacturers are closer to 60%. A study of 884 machines across 23 companies measured an average OEE of 65%.
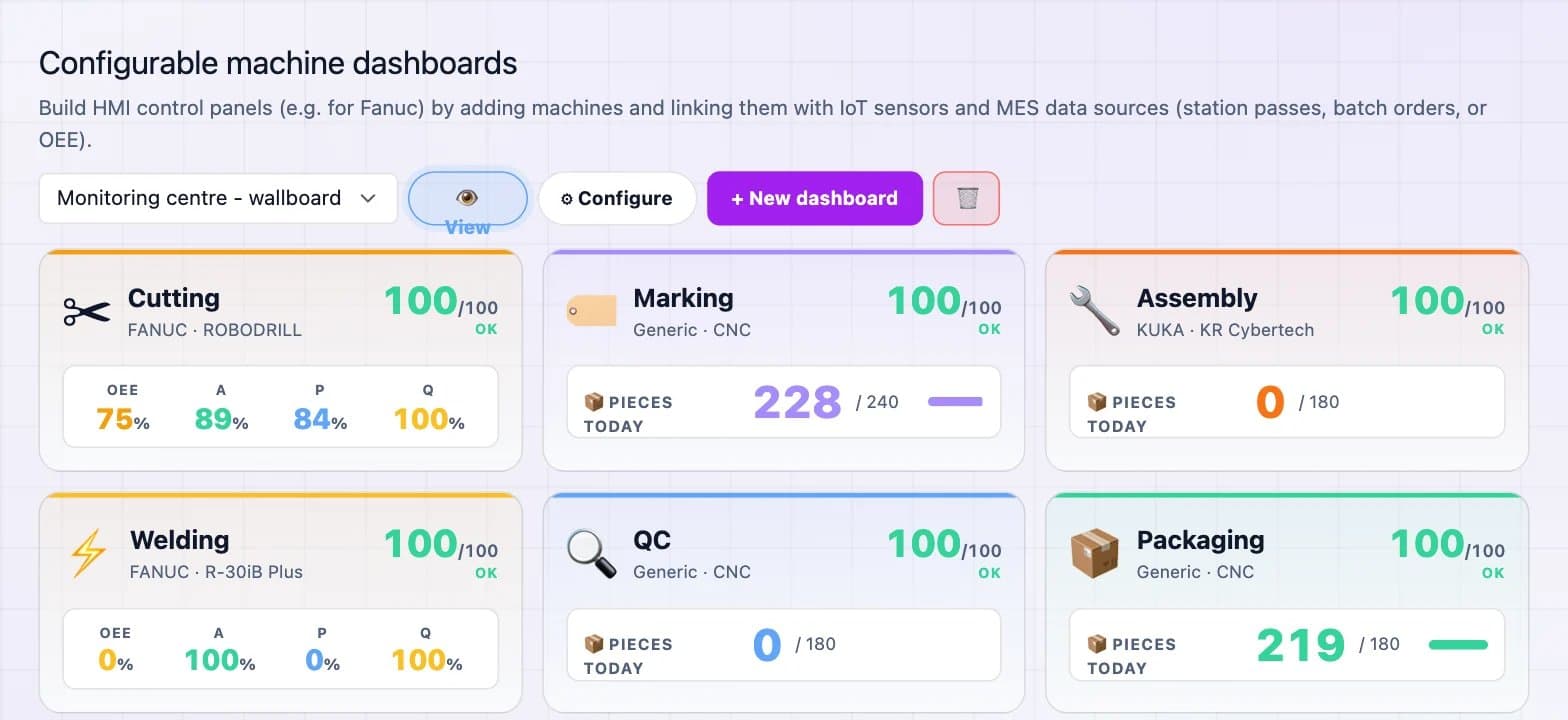
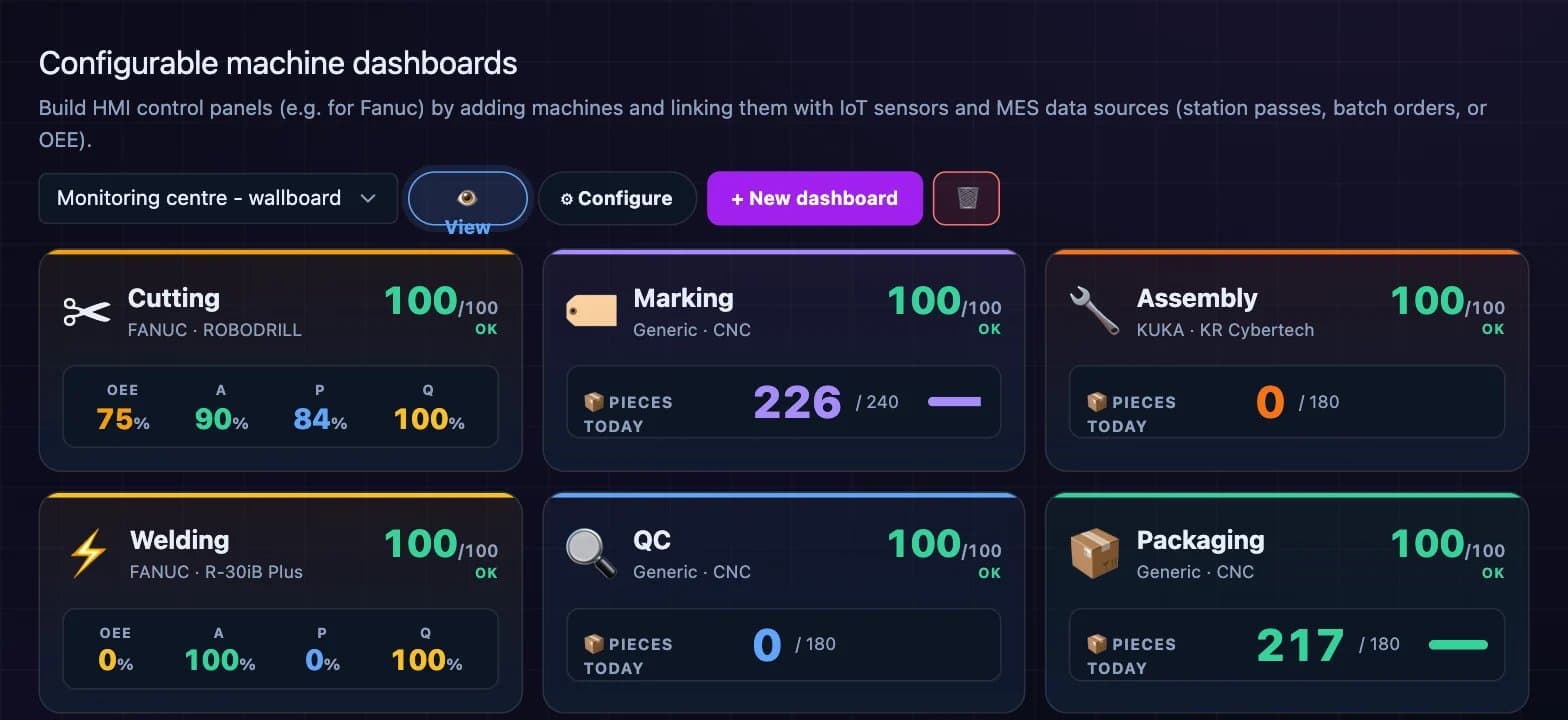
Where spreadsheet OEE goes wrong
Manual OEE goes wrong in its inputs. These five errors appear in most plants that calculate OEE by hand:
- Short stops are missing. A 90-second jam is rarely written down. Vorne notes that most companies do not accurately track idling and minor stops. They vanish into a lower performance figure with no explanation.
- The ideal cycle time is wrong. Plants often use an average or a planned rate instead of the fastest achievable cycle. That hides speed loss. If performance ever goes above 100%, Vorne points out that the ideal cycle time is set too high.
- Planned time is defined differently. One shift excludes changeovers, another excludes meetings, a third excludes "no orders". Figures that look comparable are measured against different bases. KPI frameworks such as ISO 22400 exist to make such definitions consistent.
- Reasons are guessed at shift end. Written from memory, many stops become "unknown" or "other". Even with automatic data, the Chalmers study found nearly half of recorded losses could not be classified because categories were missing or poorly described.
- Counts are copied by hand. Every transfer from a counter to paper to Excel is a chance for a typing error.
These errors follow from reconstructing a shift after it has ended, whoever fills in the sheet.
What is one OEE point worth on your line?
Enter your shifts, output and current OEE in the ROI calculator. It shows the value of every point of OEE in about three minutes.
Which of the six big losses a spreadsheet hides
Vorne groups OEE losses into six big losses: equipment failure and setup and adjustments (availability), idling and minor stops and reduced speed (performance), process defects and reduced yield (quality).
A spreadsheet catches the big ones. Long breakdowns and changeovers get written down, and scrap is counted somewhere. The losses that slip through are minor stops and reduced speed, the two performance losses. They are frequent and short, which is exactly why nobody records them.
Manual vs live OEE side by side
| Aspect | OEE from a spreadsheet | Live OEE |
|---|---|---|
| When it is available | Next day or next week | During the shift |
| Short stops | Mostly missing | Every state change time-stamped |
| Stop reasons | Written from memory at shift end | Picked at the machine in about 2 seconds |
| Ideal cycle time | Often an average or planned rate | Set once per product and checked against data |
| Planned time | Defined differently by each shift | One definition in the system |
| Effort | Hours of typing and checking every week | Calculated from machine events |
| What you can act on | Yesterday's losses | The stop happening now |
The hidden cost of manual OEE
The visible cost is time. Take an illustrative example of a two-shift line: if a shift leader spends 20 minutes per shift writing up stops, five days a week, and a CI engineer spends 4 hours a week consolidating spreadsheets, that is over 7 hours a week for one line.
The larger cost is delay. Siemens estimates that the world's 500 largest companies lose about 11% of annual revenue to unplanned downtime. A mid-size plant loses less in absolute terms, but the mechanism is the same. When OEE arrives a day later, every decision based on it is a day late as well.
Trust suffers too. When OEE depends on who filled in the sheet, meetings turn into debates about the number, the same problem we describe in machine data is useless without context.
What changed when one line went live
On one corrugated-packaging line, operators logged stops from memory at the end of the shift. "Unknown" dominated the downtime Pareto. OEE was reconstructed in a spreadsheet a day later.
The plant introduced live machine status, reason capture at the stop in about two seconds, alerts as tasks with an owner, and live OEE. After the pilot, OEE rose from 61% to 70% and average response time to a stop fell from 24 to 9 minutes. The full case is in How to Reduce Downtime with Real-Time Data.
Moving away from spreadsheets can start small, in this order:
- agree one definition of planned time and one ideal cycle time per product;
- connect the machines on one line, including older ones without a PLC;
- write a short reason list, 10 to 15 reasons per machine type;
- review the top three losses for ten minutes at the start of each shift.
Consistent definitions are also a matter of data maturity. Our article on CMMI and data maturity explains why standard processes and shared data definitions come before automation. For the next steps, see what to measure in the first 90 days of an IoT rollout.
FAQ
What is the OEE formula?
OEE equals availability × performance × quality: run time against planned time, actual output against the ideal cycle time, and good parts against total parts.
Is spreadsheet OEE always wrong?
It usually hides short stops, looks better than it is when the ideal cycle time is too slow, and is vague about reasons. It also describes yesterday's shift. Still, it beats having no OEE at all.
What is a good OEE score?
85% is often cited as world class, and many manufacturers are closer to 60%. Compare your line with its own baseline first, because a trend you trust tells you more than a benchmark.
Does an OEE calculator replace live measurement?
No. An OEE calculator is useful to understand the formula or to value one point of OEE. Live measurement gives you the inputs the calculator needs, captured as they happen.
How long does it take to move to live OEE?
One line can be connected in weeks, including older machines. Reliable reasons and definitions take a few more weeks of daily use.
Conclusion
Most of what a spreadsheet misses sits in the two performance losses, minor stops and reduced speed, and whatever it does capture reaches the team a day after the shift could have acted on it. A sensible first step is to pick one line and agree one definition of planned time and one ideal cycle time per product there. Once its machines are connected, use what to measure in the first 90 days to decide what to track.
See live OEE on a real line
In a 30-minute online demo we show how stops, reasons and OEE are captured in DBR77 IIoT, and how a pilot on your line would be measured.
Sources
- Vorne, Calculate OEE
- Vorne, The Six Big Losses
- Vorne, World-Class OEE
- Hedman, Subramaniyan, Almström (Chalmers, Procedia CIRP), Analysis of Critical Factors for Automatic Measurement of OEE, 2016
- Institute for Supply Management, The Monthly Metric: Unscheduled Downtime (summary of Siemens data), 2024
- ISO, ISO 22400-1 Key performance indicators for manufacturing operations management, 2014
- DBR77, CMMI and data maturity
- DBR77 IIoT pilot data, corrugated-packaging line (client anonymous), 2026